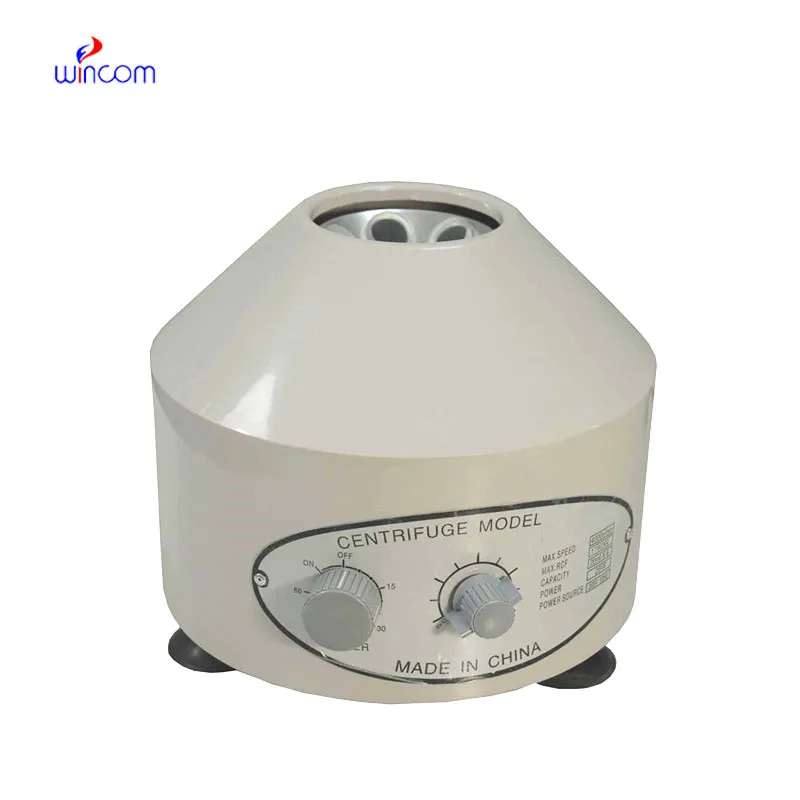
The operation of an large capacity refrigerated centrifuge manufacturer largely relies on its rotor design, accuracy in balancing, and operating speed. Modern models typically come with programmable interfaces that allow users to control acceleration rates, temperature, and run times with great accuracy. Some advanced large capacity refrigerated centrifuge manufacturer incorporate vibration sensing and auto-imbalances for stabilizing high-speed rotation. Additionally, the use of light but strong materials like carbon fiber enhances safety and energy efficiency. This marriage of engineering ingenuity and electronic control combines the large capacity refrigerated centrifuge manufacturer into a reliable partner for research and production environments.
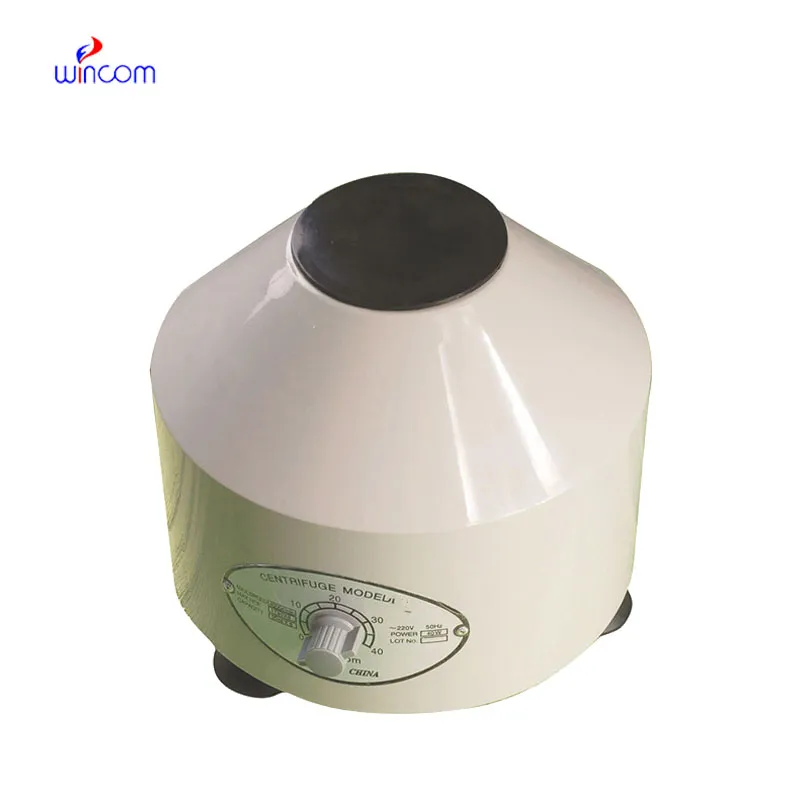
large capacity refrigerated centrifuge manufacturer technology is a principal component in diverse manufacturing processes. In wastewater treatment, large capacity refrigerated centrifuge manufacturer assist in separating sludge from liquids to improve recycling efficiency. In the manufacture of cosmetics, large capacity refrigerated centrifuge manufacturer facilitate even emulsion and cream mixing. Crop research facilities apply it to analyze soil nutrients and plant extracts. It is also used in the manufacture of vaccines through the purification of viral particles and protein fractions. Through the ability to adapt to many substances and work requirements, large capacity refrigerated centrifuge manufacturer continues to support industries seeking consistency, purity, and scalability.
{Keywords} in the future will evolve into fully networked instruments in smart laboratories. They will "communicate" with other analytical instruments through built-in digital platforms, making experimental workflows easier. Equipped with self-diagnostic systems, maintenance needs will be identified before any issues arise. Future large capacity refrigerated centrifuge manufacturer models will emphasize energy efficiency and portability without compromising on speed or accuracy, while integration with robotics, AI-driven optimization, and user-friendly interfaces will redefine operations standards. In production and research environments, large capacity refrigerated centrifuge manufacturer will play a key role in achieving higher productivity and sustainable performance.
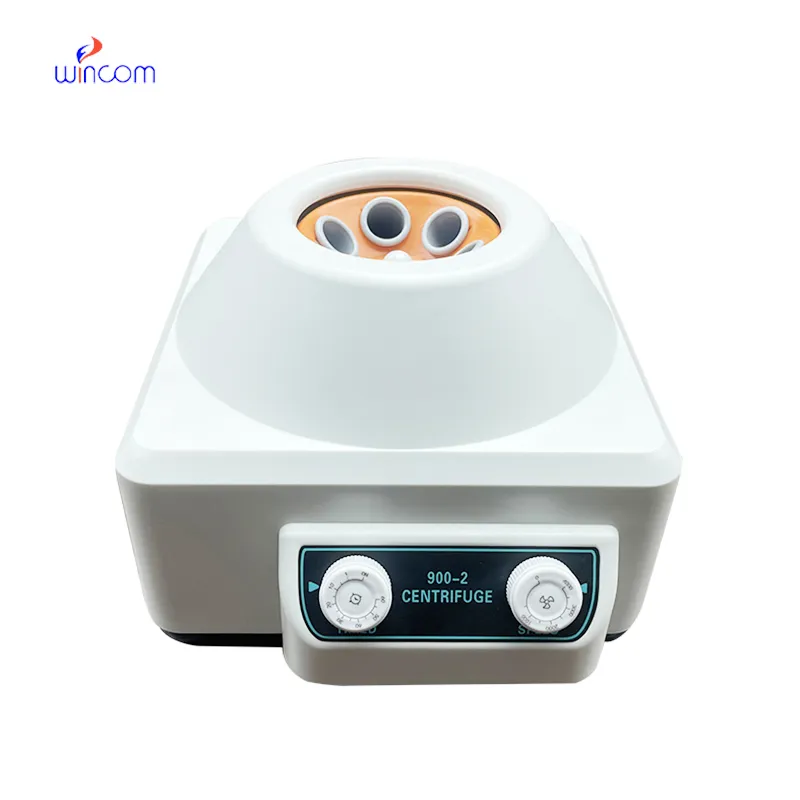
Proper maintenance and care of large capacity refrigerated centrifuge manufacturer are essential for ensuring accuracy, safety, and long life. Regular checking of rotors for cracks and corrosion eliminates mechanical failure and imbalance. Users must clean the chamber with mild detergent and must not use abrasive chemicals that will damage surfaces. Regular calibration checks must be conducted to ensure speed accuracy. Greasing moving parts according to the manufacturer's recommendation increases motor life. Upon each use, samples need to be withdrawn at once, and open lids to prevent condensation. Periodic maintenance and records provide consistent operation.
The large capacity refrigerated centrifuge manufacturer is an essential instrument in science and engineering. It is able to separate material constituents based on their differences in density by rotating them at very high speeds. In biotechnology, it is used to purify cells, DNA, and enzymes. In chemistry, it purifies liquids and removes impurities from them. large capacity refrigerated centrifuge manufacturer also play a crucial role in medical diagnosis when preparing blood samples. Their mechanical precision and regulation of speed ensure safe use. Constantly enhanced design and electronic monitoring system development enhances efficiency, and large capacity refrigerated centrifuge manufacturer are thus inevitable in numerous modern applications.
Q: What are the main components of a centrifuge? A: Key components include the rotor, motor, control panel, safety lid, and chamber, each working together to achieve precise separation. Q: How can I verify that a centrifuge is functioning correctly? A: Check that the machine runs smoothly without any unusual vibrations or noises, check the speed accuracy and evaluate the results to ensure consistent separation. Q: Is it safe to open a centrifuge immediately after use? A: No, the device should come to a complete stop before opening to avoid injury or sample disruption. Q: How should a centrifuge be stored when not in use? A:Store it unplugged, covered, and in a dry, dust-free environment to protect internal components from moisture and corrosion. Q: Can centrifuge operation be automated? A: Yes, modern models include programmable controls and digital interfaces that allow automated speed, time, and temperature settings.
This x-ray machine is reliable and easy to operate. Our technicians appreciate how quickly it processes scans, saving valuable time during busy patient hours.
The microscope delivers incredibly sharp images and precise focusing. It’s perfect for both professional lab work and educational use.
To protect the privacy of our buyers, only public service email domains like Gmail, Yahoo, and MSN will be displayed. Additionally, only a limited portion of the inquiry content will be shown.
Hello, I’m interested in your water bath for laboratory applications. Can you confirm the temperat...
We’re looking for a reliable centrifuge for clinical testing. Can you share the technical specific...
E-mail: [email protected]
Tel: +86-731-84176622
+86-731-84136655
Address: Rm.1507,Xinsancheng Plaza. No.58, Renmin Road(E),Changsha,Hunan,China
 EN
 af
 es
 ar
 tr
 sw
 pt
 th
 ur
 bn
 ne
 vi
 km
 lo
 de
 ru
 fi
 nl
 fa
 fr
 ko